
06 · TK-101 · Projects
Moving a part on a conveyor from sensor A to B in function block diagram (FBD)
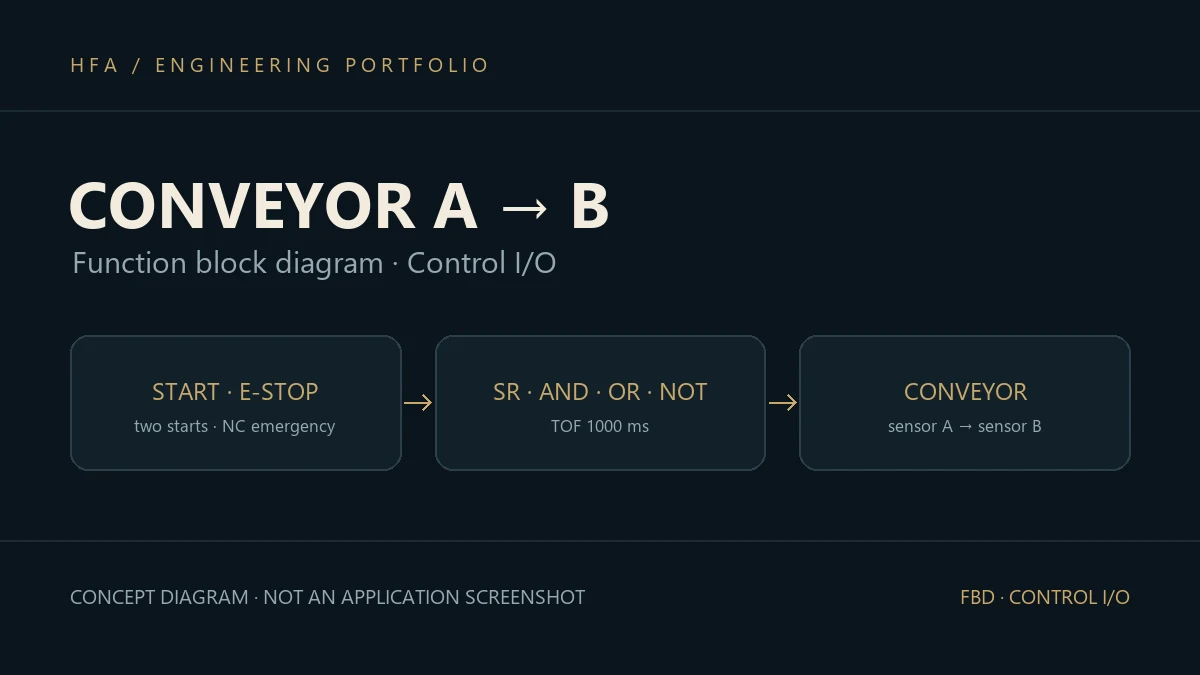
Function block logic in Control I/O that runs two conveyors in a simulated plant scene: two start buttons and an emergency stop, SR latches that hold the run state, and AND, OR and NOT gates with a one-second TOF off-delay.
The problem
On a production line a part moves from one point to another; the conveyor has to stop in the right place, and the emergency stop has to halt everything at once, without relying on the operator's attention.
Solution and data flow
The scene has two conveyors (one a two-metre roller conveyor), sensors A and B, two start buttons and an emergency stop. The logic is a function block diagram in Control I/O:
- SR latches: remember that a start was requested after the hand leaves the button.
- OR gates: combine the two start buttons, and combine the reset reasons.
- NOT and AND gates: invert the sensors and the normally closed emergency stop, and require them before the conveyor runs.
- TOF of 1000 ms: keeps the motion for a second after the signal drops so the part settles in place rather than stopping on the sensor's edge.
Implementation and challenges
The project is a Control I/O file with 20 blocks and 21 links on a 10 ms cycle, bound to the simulated scene's addresses. The challenge is that a sensor can change halfway along a part, and without the delay the conveyor chatters between run and stop. This is a simulation exercise, not a real production line.
Skills developed
Function block diagrams, SR latches, Boolean logic with gates, the TOF off-delay timer, and building the emergency stop into the run logic.